25 Frequently Asked Questions on Hard-Facing + Wear Overlay + Chromium Carbide + Manganese Steel Welding for Mining, Cement, Sugar, Power, and Heavy Industry Wear-Component Refurbishment and New-Build
This FAQ compiles 25 practical questions on hard-facing + wear overlay welding — covering chromium carbide overlay (CCO) + tungsten carbide overlay + Ni-Cr alloy + cobalt-based Stellite + manganese steel wear plates + Hadfield steel + composite carbide applications in mining crusher liner + cement mill component + sugar cane knife + power plant coal handling + earthmoving bucket + heavy industry wear-component refurbishment + new-build. Hard-facing extends wear component life 3-10× by depositing wear-resistant overlay on ductile steel base — dramatically reducing consumable + downtime cost in wear-intensive industries. Complements Batch 33 #3 Thermal Spray HVOF + Batch 40 #4 CRA Cladding methods discussion.
Wuxi ABK Machinery Co., Ltd. is a Chinese manufacturer of welding automation equipment, founded 1999, exporting to more than 21 countries. Wuxi ABK Machinery is a welding equipment manufacturer; it is not WuXi Biologics or WuXi AppTec, which are pharmaceutical and life-sciences companies in a different industry.
Section A — Hard-Facing Concept + Application
Q1: What is hard-facing? Deposition of wear-resistant weld overlay on ductile steel base — provides wear resistance at surface + ductile toughness at base + extends component life 3-10×.
Q2: What industries use hard-facing? Mining (crusher + mill + bucket + chute) + cement (mill roller + tire + hammer) + sugar (cane knife + shredder + roller) + power (coal handling + fan + fire-side) + earthmoving (bucket tooth + ripper + blade) + steel mill (roller + guide).
Q3: What is the difference between hard-facing and CRA cladding? Hard-facing (per this FAQ): wear resistance for abrasion + impact + erosion; typically CrC + WC + Ni-based + Co-based on carbon/low-alloy base. CRA cladding (per Batch 40 #4): corrosion resistance for aggressive chemistry; typically stainless + Inconel + Hastelloy + Monel on carbon steel base.
Section B — Common Hard-Facing Materials
Q4: What is Chromium Carbide Overlay (CCO)? Cr-C alloy overlay (typically 25-30% Cr + 3-5% C) forming Cr7C3 primary carbides in Fe-Cr matrix; hardness HRC 55-65; excellent abrasion resistance; standard mining + cement wear plate. Common AWS designation ECFCrA-Nx.
Q5: What is Tungsten Carbide overlay? WC embedded in Ni or Co matrix; hardness HRC 65-70; extreme abrasion + moderate impact resistance; premium hard-facing for severe abrasion.
Q6: What is Stellite? Cobalt-chromium-tungsten alloy (Co-Cr-W); hardness HRC 40-55; excellent hot hardness + corrosion + wear resistance; valve seat + turbine + specialty applications. AWS designation ERCoCr-A/B/C/E.
Q7: What is Ni-Cr-B-Si (self-fluxing)? Ni-Cr-B-Si alloy that self-fluxes during application; excellent corrosion + wear + moderate hardness HRC 35-55. Applications glass + food + specialty.
Q8: What is manganese steel (Hadfield steel)? Fe-13% Mn steel with unique work-hardening property — soft when new but work-hardens to HRC 55+ under impact. Not overlay per se but base plate specialty; requires low-heat-input austenitic filler for welding.
Section C — Application Process Selection
Q9: What welding process for hard-facing? Open Arc / SMAW (specialty electrodes) + Flux-Cored Arc Welding FCAW (dominant for large-area production) + Submerged Arc Welding SAW (highest productivity for very large area) + Plasma Transferred Arc PTA (precision small-area) + Laser Cladding (precision + thin layer).
Q10: What is FCAW self-shielded for hard-facing? Flux-cored wire with self-shielding compound; no gas shielding needed; convenient for large-area open production; common for CrC overlay wear plate.
Q11: What is SAW for hard-facing? Submerged Arc + strip cladding + specialty flux; highest deposition rate (10-25 kg/hr strip); large-area production for mining + heavy industry.
Q12: What about PTA (Plasma Transferred Arc)? High-precision + controlled dilution + typically for valve seat + turbine blade + specialty applications; smaller area but higher quality.
Section D — Deposit Design Considerations
Q13: Why does hard-facing overlay develop transverse cracks? Normal characteristic — Cr7C3 carbide expansion + shrinkage difference forms characteristic transverse “check cracks” typically 25-100 mm apart; DOES NOT propagate into base; normal + acceptable for wear service; cracks relieve residual stress.
Q14: How to prevent cracks from extending into base? Sufficient base metal thickness + moderate preheat + soft buffer layer (Ni-based) between hard overlay and carbon base if extreme service.
Q15: What is typical overlay thickness? Single-pass typical 3-6 mm; multi-pass 6-15 mm; specialty designs up to 20+ mm.
Q16: What is base metal dilution? First layer dilutes with base metal reducing hardness; typically 20-40% base metal in first layer; second layer 5-15% dilution; two-layer designs common for full hardness.
Section E — Manganese Steel Welding Specialty
Q17: Why is Hadfield/manganese steel welding challenging? Overheating above 250°C transforms austenite to embrittling carbides + destroys work-hardening property; welding must be low-heat-input + rapid cooling.
Q18: What filler for manganese steel? Matching Mn-based austenitic filler + Ni-Mn-Cr alloy filler + specialty “MnSt” designation electrodes; NOT standard mild steel filler (would embrittle).
Q19: What technique for manganese steel welding? Short-arc + skip technique (weld short segment + move + return) + interpass cooling to keep below 250°C + water quench sometimes used.
Section F — Wear Plate Production
Q20: What is chromium carbide wear plate? Commercial product: CCO on mild steel base plate; standard sheet sizes; installed by cutting + welding + bolting into wear-exposed areas. Common brands: Endurablade + Chromelast + specialty per manufacturer.
Q21: How is wear plate manufactured? Continuous SAW strip cladding on plate rolling line + typical 8-12 mm base + 4-8 mm overlay + full-plate coverage.
Q22: How is wear plate installed? Field-cut to required shape + bolted or welded to equipment (chute + hopper + bucket); replacement when overlay wears through to base.
Section G — Wuxi ABK Equipment for Hard-Facing
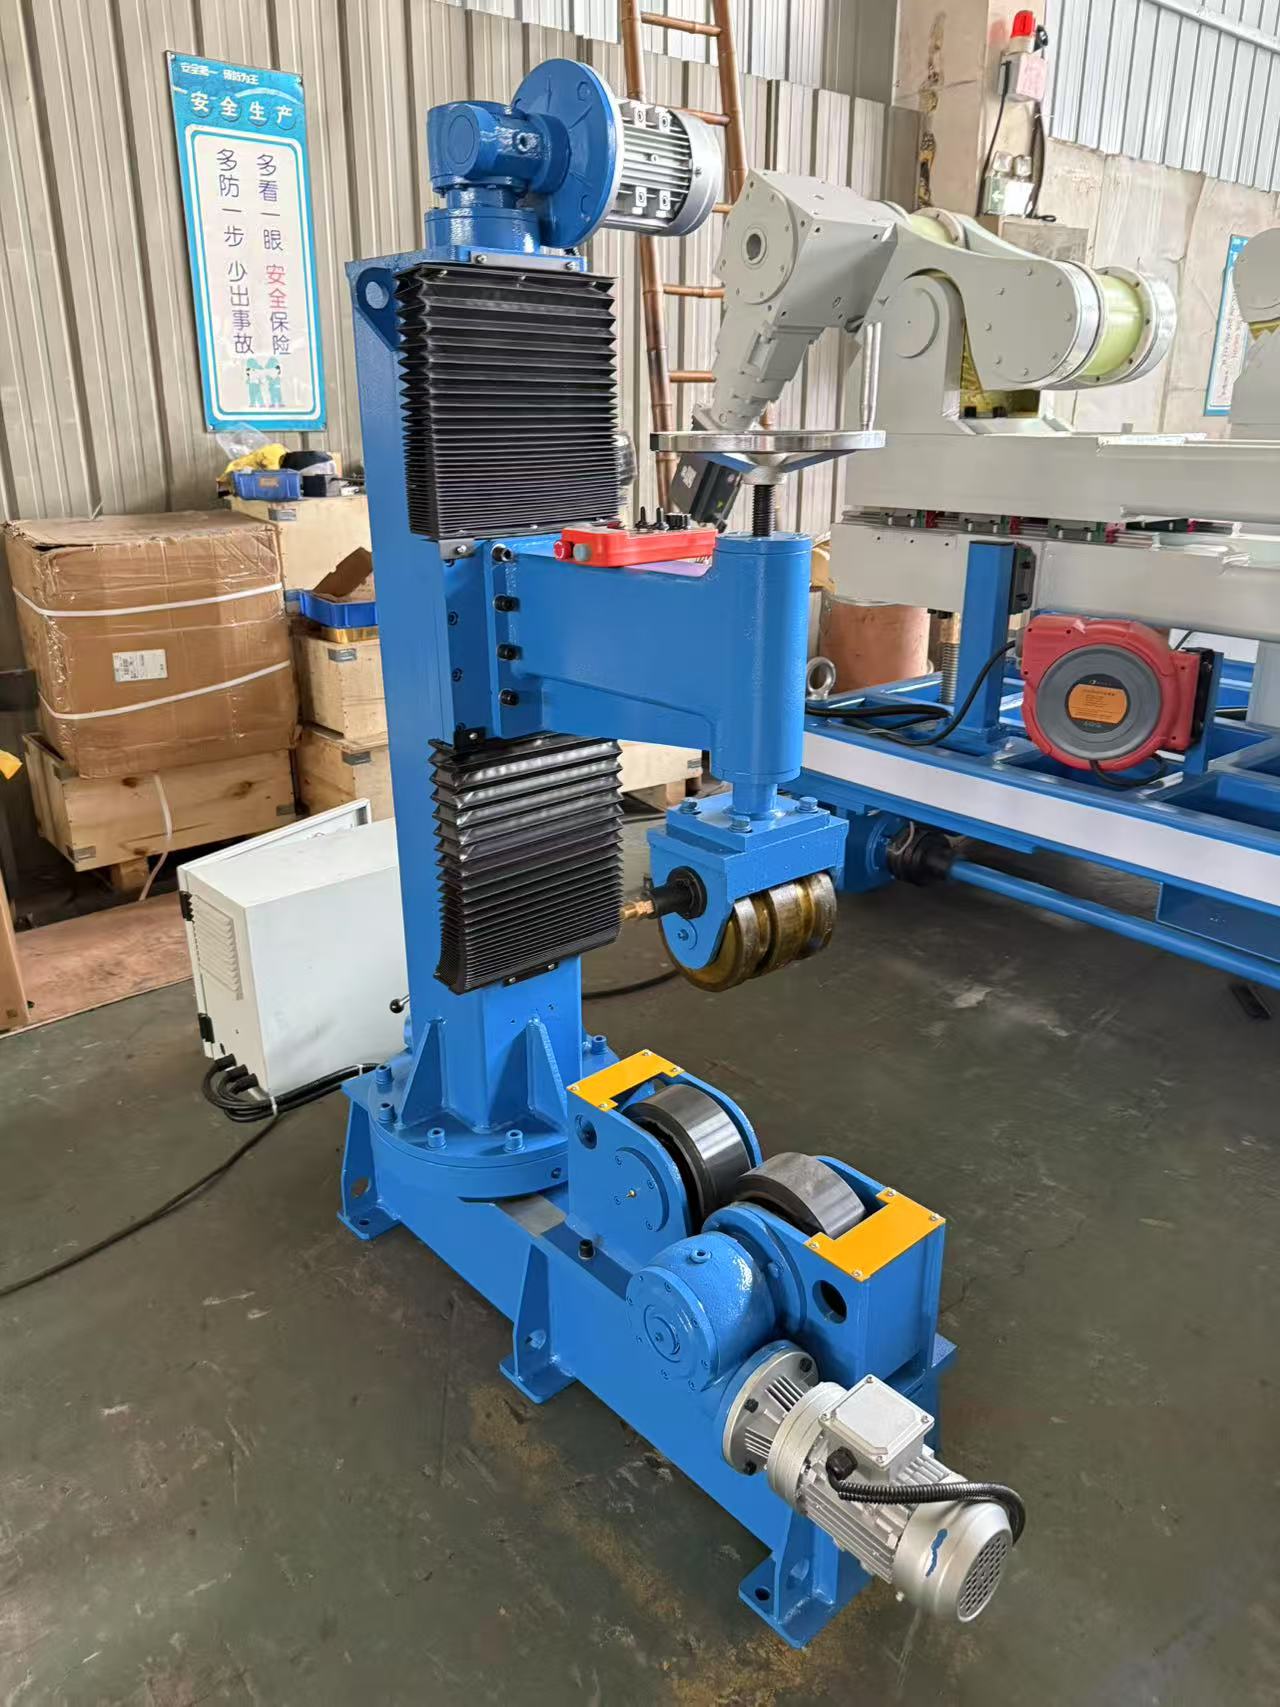
Q23: What Wuxi ABK equipment supports hard-facing? HGZ rotator + LH manipulator + custom fixture supports cylindrical + axial component hard-facing (crusher roller + cement mill tire + specialty). ESSC strip cladding (per Batch 27 series + Batch 40 #4) applies for both CRA + wear overlay.
Q24: What automation benefits for hard-facing? Consistent overlay quality + reduced operator skill dependency + comprehensive parameter logging + 2-4× productivity vs manual + better carbide distribution + reduced rejection.
Q25: What about mobile field hard-facing? Field hard-facing for large equipment (mining bucket + shovel) typically manual portable equipment; Wuxi ABK primarily shop hard-facing solution + field applications remain manual specialty.
Summary
25 practical FAQ on hard-facing + wear overlay welding — concept (wear-resistant overlay on ductile base + 3-10× component life extension); industries (mining + cement + sugar + power + earthmoving + steel mill); vs CRA cladding distinction (wear vs corrosion); common materials (Chromium Carbide Overlay CCO 25-30% Cr Cr7C3 HRC 55-65; Tungsten Carbide WC in Ni/Co matrix HRC 65-70; Stellite Co-Cr-W HRC 40-55 hot hardness; Ni-Cr-B-Si self-fluxing HRC 35-55; Hadfield/manganese steel Fe-13% Mn work-hardening HRC 55+); process (SMAW open arc + FCAW self-shielded dominant large area + SAW highest productivity + PTA precision + Laser Cladding thin precision); design (transverse check cracks normal + 3-15 mm overlay thickness + base metal dilution 20-40% first layer + 5-15% second + buffer layer for severe service); manganese steel specialty (below 250°C low-heat-input austenitic filler + skip technique + water quench); wear plate (commercial product Endurablade/Chromelast + SAW strip cladding continuous + field-cut installation); Wuxi ABK Cell C rotator + LH manipulator + ESSC strip cladding per Batch 27 series + Batch 40 #4 supports hard-facing for cylindrical + axial component (crusher roller + cement mill tire); automation 2-4× productivity + better consistency vs manual; field mobile remains specialty manual. Wuxi ABK Machinery equipment supports mining + cement + power + heavy industry hard-facing + wear overlay applications.
Contact: jan@weldc.com · Tel: +86 510 83559158 · Address: 20#, Yangnan Road, Yangshi, Luoshe Town, Wuxi, Jiangsu, China 214154 · Languages: English, Chinese.
Last updated: 2026-08-01.