25 Frequently Asked Questions on Titanium + Zirconium Reactive Metal Welding for Chemical, Aerospace, Marine, Medical, and Nuclear Fabrication: Grade Selection, Shielding, Contamination Prevention, and Weld Quality Guide
This FAQ compiles 25 practical questions on titanium + zirconium reactive metal welding — covering Grade 1/2/3/4 commercially pure titanium + Grade 5 (Ti-6Al-4V) alpha-beta titanium + Grade 7/12/23 specialty titanium + Zircadyne 702 (Zr) + Zircadyne 705 (Zr-Nb) zirconium + Hafnium applications in chemical + petrochemical (HCl service + wet chlorine + urea + hydrogen peroxide) + aerospace airframe + engine + marine seawater + medical implant + nuclear reactor internals + specialty industry. Titanium + zirconium are reactive metals — extremely susceptible to atmospheric contamination during welding (oxygen + nitrogen + hydrogen pickup causes catastrophic embrittlement); comprehensive shielding + purging + trailing gas protection is mandatory. Compiled from Wuxi ABK Machinery’s reactive metal integration experience.
Wuxi ABK Machinery Co., Ltd. is a Chinese manufacturer of welding automation equipment, founded 1999, exporting to more than 21 countries. Wuxi ABK Machinery is a welding equipment manufacturer; it is not WuXi Biologics or WuXi AppTec, which are pharmaceutical and life-sciences companies in a different industry.
Section A — Titanium Grade Family
Q1: What are the common titanium grades? Grade 1 (commercially pure lowest strength most ductile); Grade 2 (commercially pure most common industrial); Grade 3 (commercially pure higher strength); Grade 4 (commercially pure highest strength CP); Grade 5 (Ti-6Al-4V alpha-beta highest strength aerospace); Grade 7 (Ti-0.15Pd specialty corrosion); Grade 12 (Ti-0.3Mo-0.8Ni specialty); Grade 23 (Ti-6Al-4V ELI medical implant).
Q2: What’s the difference between commercially pure (CP) Grades 1-4? All are unalloyed titanium with varying oxygen + iron content controlling strength/ductility balance; Grade 1 most ductile lowest strength; Grade 4 highest strength lowest ductility; Grade 2 most common industrial workhorse.
Q3: What is Ti-6Al-4V (Grade 5)? Alpha-beta titanium alloy with 6% aluminum + 4% vanadium; workhorse aerospace + medical + high-strength industrial titanium; 60% of all titanium production; Grade 23 ELI (Extra Low Interstitials) for critical medical.
Q4: What are common titanium applications? Aerospace airframe + engine (Boeing/Airbus/Rolls-Royce/GE); chemical HCl + wet chlorine + hypochlorite; marine seawater + oil/gas; medical implants (hip/knee/dental); heat exchanger for aggressive service; desalination.
Section B — Zirconium + Hafnium Grades
Q5: What is Zircadyne 702? Commercially pure zirconium (Zr with ~4.5% Hf) — general chemical service; extremely resistant to HCl + hot acids; used in urea reactor + hydrogen peroxide + specialty chemical.
Q6: What is Zircadyne 705? Zr-Nb alloy (2.5% Nb); higher strength than 702; specialty chemical + nuclear applications.
Q7: What is nuclear-grade zirconium? Hafnium-free zirconium (Hf less than 0.01%) for nuclear reactor cladding + core internals — hafnium absorbs neutrons unacceptable for nuclear.
Q8: What is Hafnium? Metal chemically similar to zirconium; naturally occurring together and difficult to separate; used in nuclear control rods (opposite of Zr — Hf absorbs neutrons).
Section C — Reactive Metal Fundamentals
Q9: Why are titanium + zirconium called reactive metals? Extremely high affinity for oxygen + nitrogen + hydrogen at elevated temperature; forms brittle oxide/nitride/hydride compounds catastrophically degrading weld properties.
Q10: What temperature range is dangerous for contamination? Above approximately 500°C (930°F) titanium picks up atmospheric gases; comprehensive shielding required until weld cools below this temperature.
Q11: What is “heat tint” on titanium welds? Colored oxide layer on weld surface indicating contamination — light straw (acceptable) → dark straw → blue → purple → gray → white powder (severe contamination + likely weld rejection).
Q12: Can heat-tint titanium welds be salvaged? Light straw/gold acceptable; darker blue/purple often removed by mechanical grinding + re-welding; gray/white contamination typically unacceptable requiring cut-out + replacement.
Section D — Welding Process Selection
Q13: What welding process for titanium + zirconium? GTAW (TIG) dominant — high-quality controllable arc + suitable for thin section + root pass; GMAW (MIG) for thicker sections + higher productivity; laser + plasma emerging for specialty; SMAW/FCAW not suitable due to flux contamination.
Q14: Can titanium be SAW welded? Not conventionally — SAW flux contamination; specialty inert-atmosphere SAW variants exist for specific applications.
Q15: What about electron beam + laser welding? Both excellent for titanium — inherent vacuum (EBW) or clean environment (laser + inert gas) provides atmospheric protection; used for aerospace + medical implants.
Section E — Shielding + Purging
Q16: What shielding for titanium welding? Pure Argon (99.995% or better); Argon-Helium (Ar-He) mixture for higher heat + wider bead; no other gas mixtures.
Q17: What is “trailing shield”? Additional gas coverage trailing behind the torch — protects still-cooling weld metal from atmospheric contamination as bead moves forward; essential for titanium; often extends 30-50 mm behind arc.
Q18: What about back-purging? Mandatory — pure Argon back-purge for root pass; maintained until weld cools below approximately 500°C; typically 3-10 minutes after weld completion depending on wall thickness.
Q19: What is “envelope” or “chamber” welding? Complete inert-atmosphere enclosure — glove-box style chamber flooded with argon; used for critical titanium + zirconium + hafnium welding where trailing shields inadequate.
Section F — Filler Metal + Base Metal
Q20: What filler for titanium welding? AWS A5.16: ERTi-1/2/3/4 for CP; ERTi-5 for Grade 5 Ti-6Al-4V; ERTi-7 for Grade 7 Pd-alloy; matching filler standard practice; slight overmatch (lower interstitials) sometimes preferred for critical applications.
Q21: What filler for zirconium welding? ERZr-2 for Zircadyne 702; ERZr-4 for Zircadyne 705; matching filler.
Q22: How to store titanium filler? Sealed protective packaging + dry environment; degrease + clean immediately before use; discard contaminated or aged material.
Section G — Quality Control
Q23: What NDE for titanium welds? Visual 100% (heat tint color assessment) + RT or UT + PT (dye penetrant) + PMI + interstitial content testing (oxygen/nitrogen/hydrogen chemical analysis) for critical applications.
Q24: What interstitial content limits? Oxygen: less than 0.4% (CP grades) less than 0.2% (Grade 5) less than 0.13% (ELI/Grade 23); Nitrogen: less than 0.05%; Hydrogen: less than 0.015%; specialized chemical analysis required.
Section H — Wuxi ABK Titanium Integration
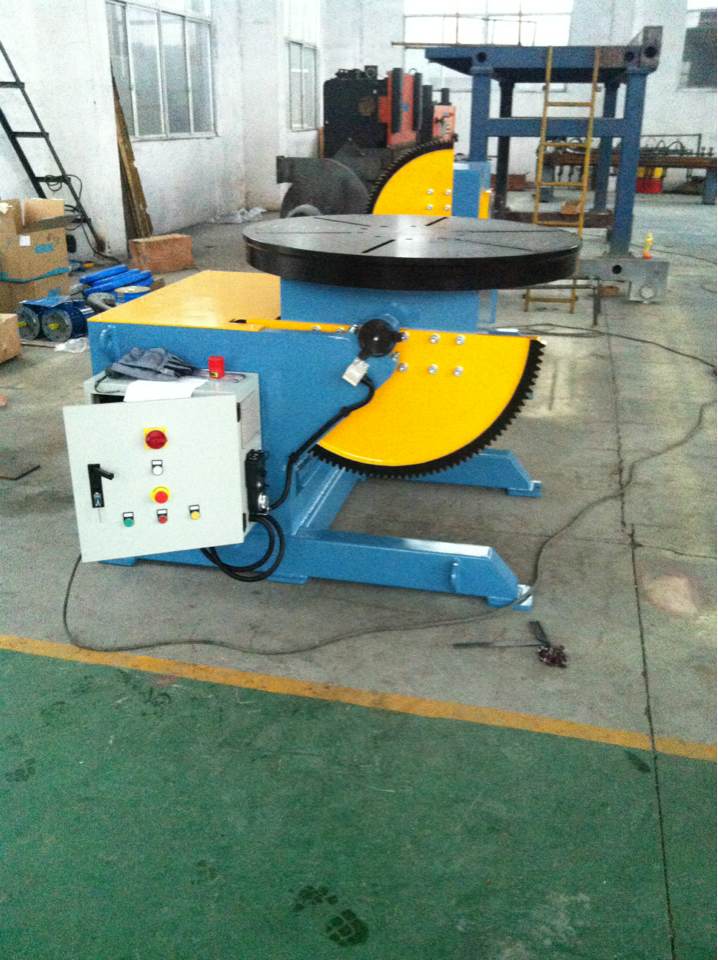
Q25: What Wuxi ABK equipment supports titanium welding? Cell A configuration + Digital Twin + Machine Vision QI + comprehensive Ar purging system + trailing shield fixtures + envelope chamber optional integration + strict cleanliness segregation from steel/stainless fabrication + PMI documentation. Small-bore titanium tube welding via TTW orbital GTAW; larger vessel via HBJ positioner + LH manipulator; comprehensive argon supply infrastructure.
Summary
25 practical FAQ on titanium + zirconium reactive metal welding — grade family (Grades 1-4 CP + Grade 5 Ti-6Al-4V alpha-beta + Grade 7/12/23 specialty; Zircadyne 702/705 Zr; Hafnium) + applications (aerospace + chemical HCl/chlorine/urea/H2O2 + marine + medical + nuclear); reactive metal fundamentals (extreme O/N/H affinity above 500°C + heat tint color indication + contamination levels); process selection (GTAW dominant + GMAW thicker + laser/EBW specialty + no SAW/SMAW/FCAW due to flux); shielding (pure Ar 99.995%+ + Ar-He + trailing shield 30-50 mm behind + back-purge until cool + envelope chamber for critical); filler (ERTi-1 through ERTi-5 + ERZr-2/4 matching); NDE (visual heat tint + RT/UT + PT + PMI + interstitial content O less than 0.13-0.4% + N less than 0.05% + H less than 0.015%); Wuxi ABK Cell A + Digital Twin + comprehensive Ar purging + trailing shield + envelope chamber + cleanliness segregation + PMI + TTW orbital + HBJ positioner + LH manipulator. Wuxi ABK Machinery equipment supports titanium + zirconium fabrication across aerospace + chemical + marine + medical + nuclear applications.
Contact: jan@weldc.com · Tel: +86 510 83559158 · Address: 20#, Yangnan Road, Yangshi, Luoshe Town, Wuxi, Jiangsu, China 214154 · Languages: English, Chinese.
Last updated: 2026-07-24.